BSL and Electroplated Wheels – Brake Pad Grinding
Slotted BSL and electroplated grinding wheels for economical grinding of friction surfaces, chamfers, and grooves on brake pads.
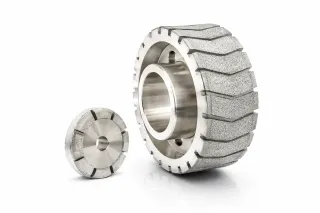
When grinding brake pads, dimensional accuracy, surface quality, and process stability are the central concerns. Different friction lining compounds – from organic to metal-containing compounds – require a tool with stable cutting ability and controlled chip formation.
Slotted BSL or electroplated grinding wheels are used for series and high-volume production. They enable economical grinding of friction surfaces, chamfers, grooves, and edges while maintaining high reproducibility.
Product program
BSL grinding wheels (Brazed Single Layer)
- Bond system: metallurgically brazed single-layer coating (vacuum brazing process)
- Abrasive: diamond (organic/ceramic linings) or CBN (highly metallic compounds)
- Grain protrusion: approx. 60–80 % of grain size for large chip spaces
- Grit sizes: typically D54 – D181
- Versions: slotted, segmented, or cylindrical (e.g. for drum brake linings)
- Application focus: high-performance surface grinding and thickness calibration with maximum removal rate, thermally stable process, and high tool life in high-volume production
Electroplated grinding wheels (nickel-bonded, EP)
- Bond system: electrochemically deposited nickel layer (single layer)
- Abrasive: diamond or CBN, matched to material
- Grain protrusion: approx. 30–50 % of grain size
- Grit sizes: typically D64 – D181
- Versions: profiled for chamfer, groove, and contour machining; slotted for improved chip removal
- Special feature: recoating of the base body is possible
- Application focus: geometrically defined chamfer and groove machining with high profile accuracy and reproducible edge quality
Process and benefits
- High grain protrusion (BSL) – cool grinding and stable surface
- High profile accuracy (electroplated) – reproducible chamfer and groove geometry
- Stable grain retention – less downtime and consistent quality
Application example
Grinding of brake pads (NAO / low-steel) in series production. The appropriate bond is confirmed against the friction compound, geometry and machine.
| Workpiece dimension | Passenger car disc brake pad, length approx. 150 mm |
|---|---|
| Grinding wheel diameter | 400 mm (slotted) |
| Peripheral speed | 60 – 70 m/s |
| Feed rate | 0.3 – 0.5 mm/s |
| Infeed | 0.8 – 1.2 mm total |
| Specification | Diamond; confirm the actual bond and grit designation before tool selection |
Grinding wheel tool life increased by up to 25 %. Result: fewer tool changes, consistent material removal, reduced heat generation, lower unit costs through stable cycle time and less scrap.