Match turning and milling to the component
EHWA offers PCBN tools for machining heat-treated steel components of constant-velocity joints. The EBC52X grade supports continuous and interrupted turning. PCBN endmills complement the range for cutting the joint geometry.
EHWA describes cutting as an increasingly used alternative to grinding in CV-joint machining and develops precise, high-quality endmills for these applications. The appropriate process sequence depends on the component, material condition and surface requirements.

EBC52X for heat-treated steel
EBC52X is a high-content PCBN grade developed by EHWA for continuous and interrupted cutting of heat-treated CV-joint steel. EHWA describes high performance even under demanding machining conditions. The product sheet does not quantify the CBN content.
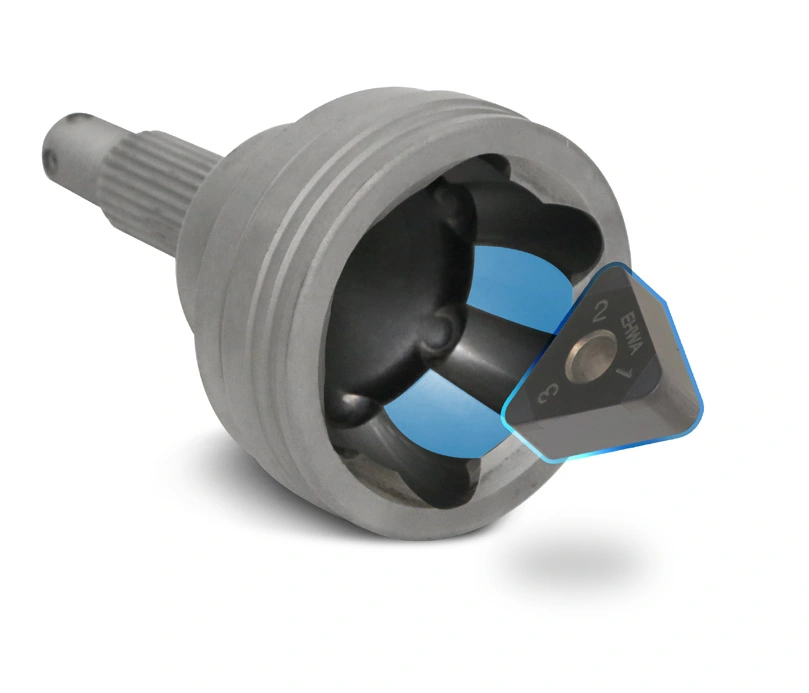
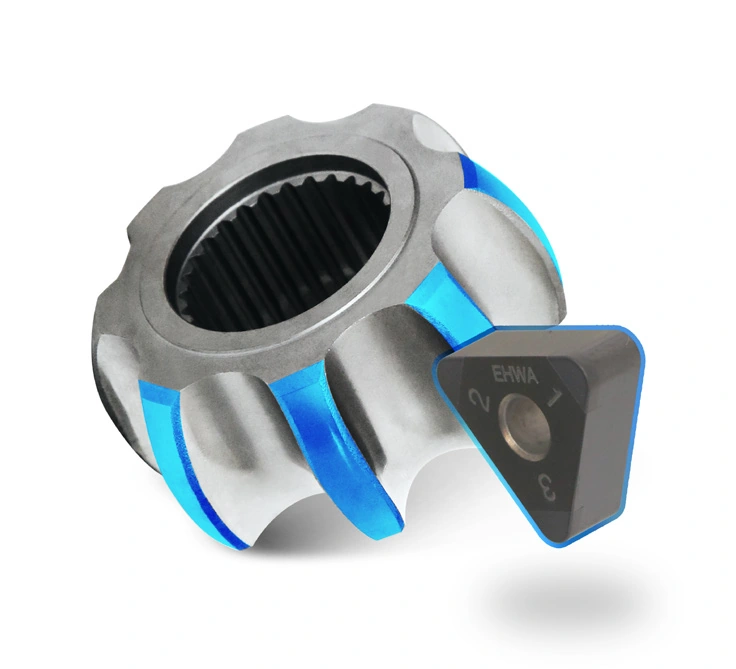
Two complete turning examples
| Parameter | Outer race turning | Inner race turning |
|---|---|---|
| Workpiece | Forged steel | Forged steel |
| Cutting speed | 120 m/min | 200 m/min |
| Feed rate | 0.10–0.12 mm/rev | 0.20 mm/rev |
| Depth of cut ap | 0.10–0.20 mm | 0.09–0.15 mm |
| Coolant arrangement | Dry | Dry |
| Cut | Interrupted | Interrupted |
The examples compare EBC52X with an unspecified competitor tool. EBC52X has the higher bar in both charts. The outer-race axis shows 0, 200, 400 and 600; the inner-race axis shows 0, 100, 200, 300 and 400. The document gives neither an axis unit nor exact bar values. The comparison retains the geometry and original scales.
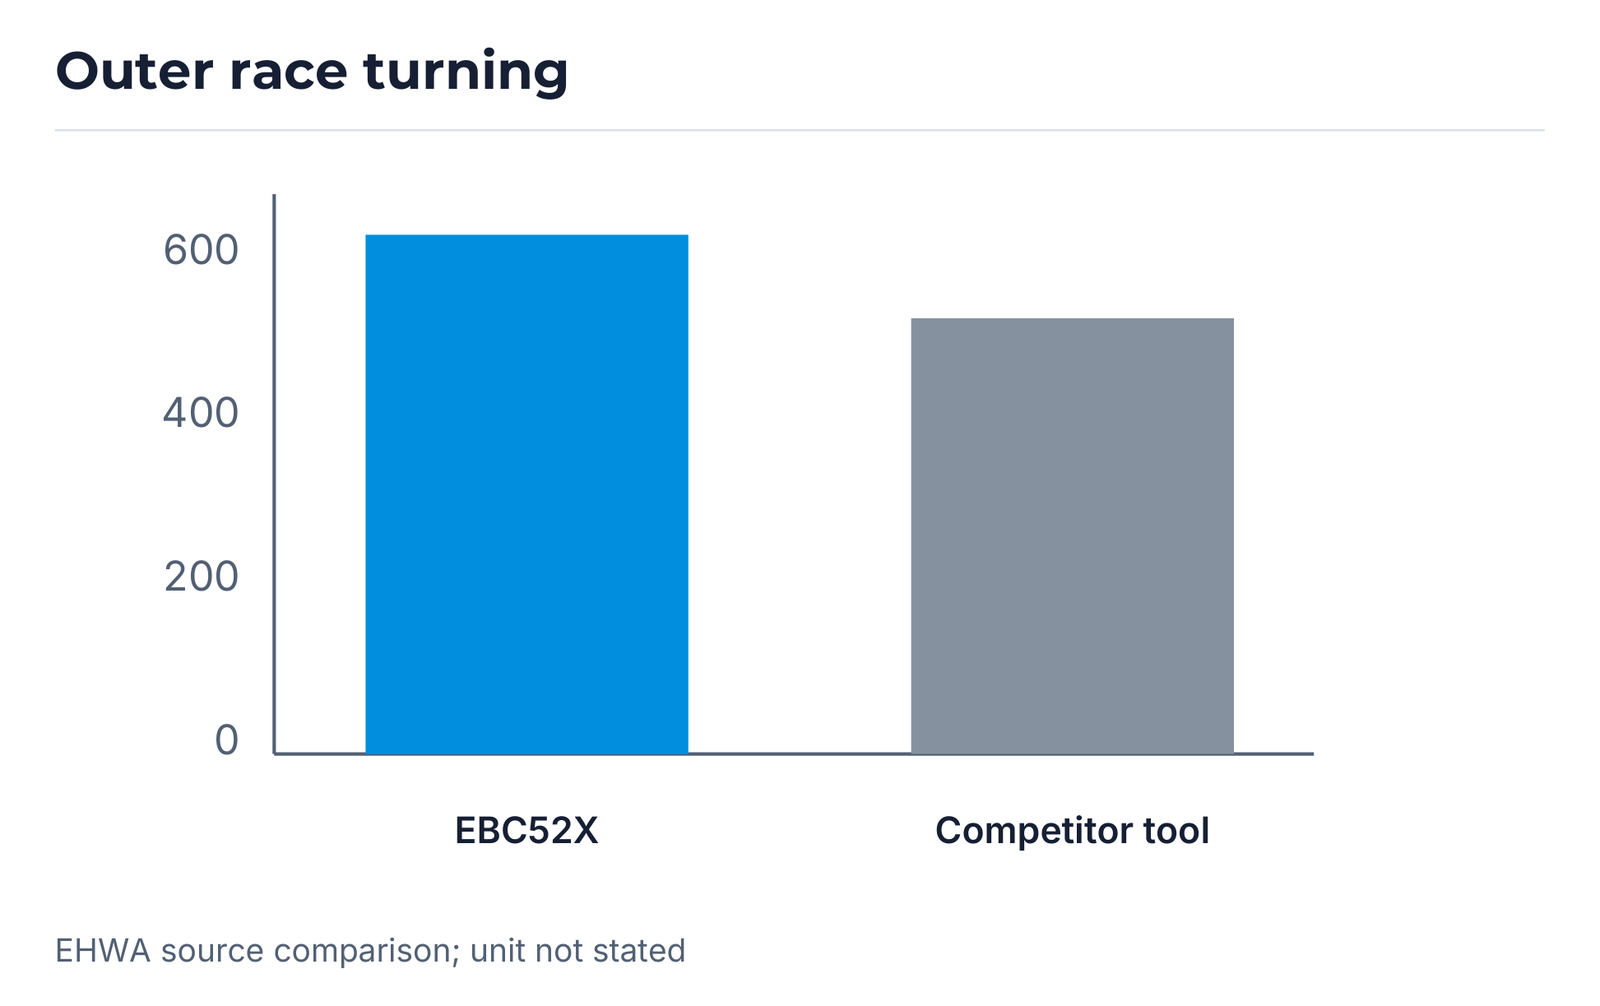
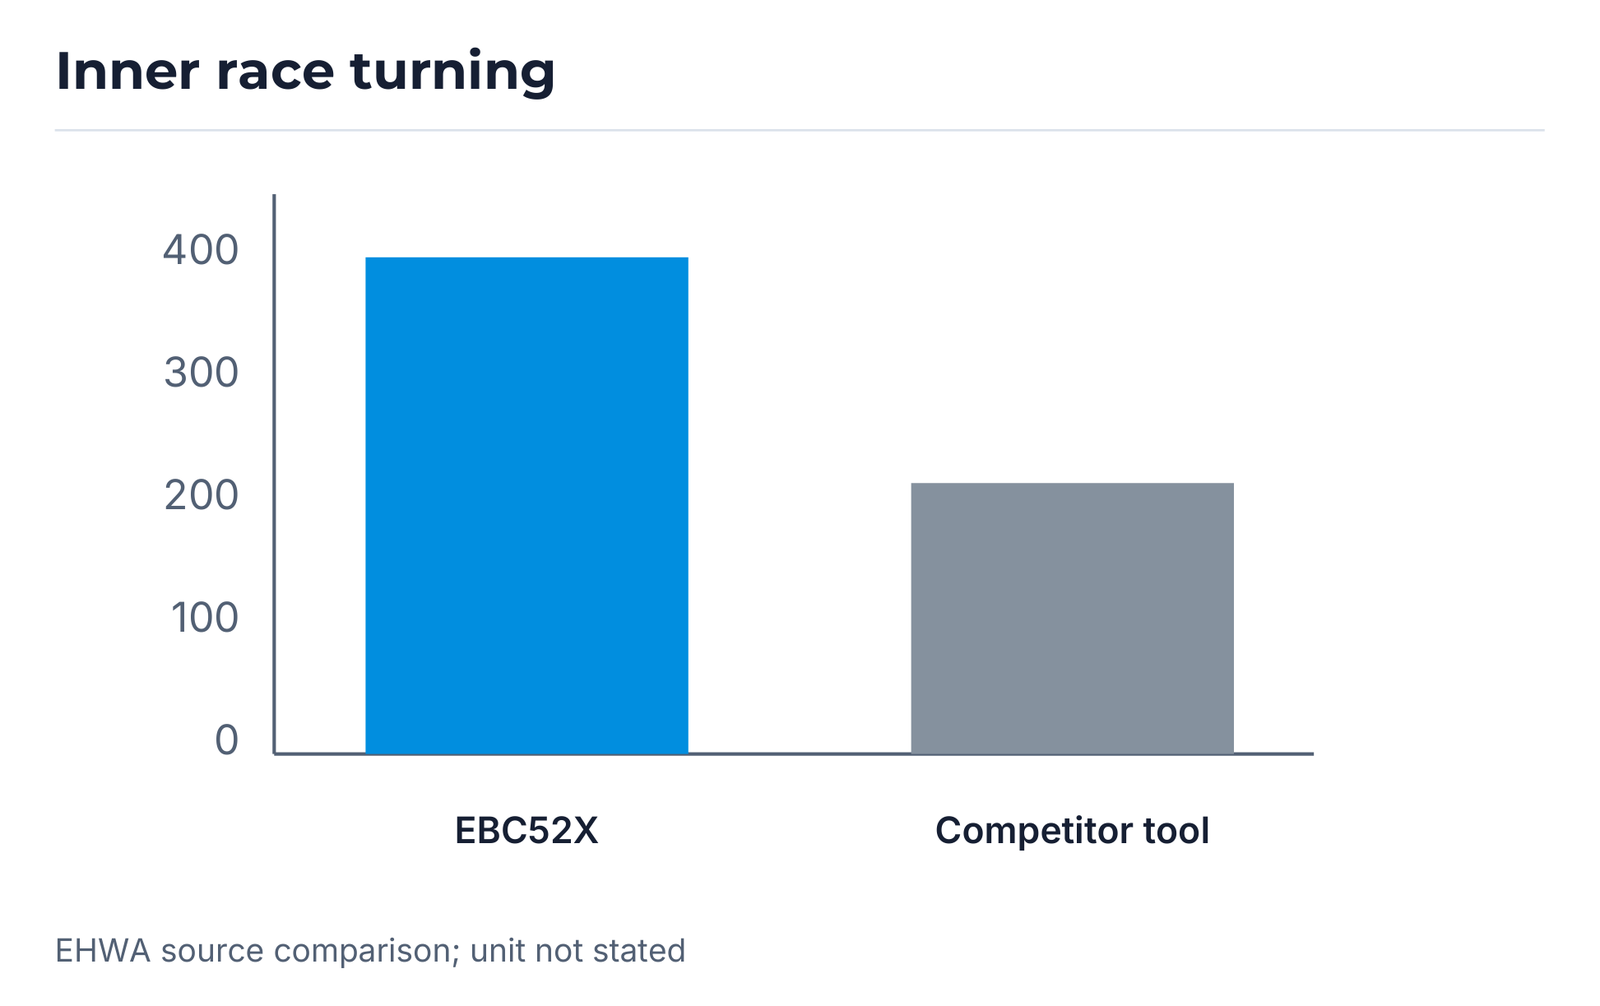
The cutting data describe the two stated applications. Material condition, cutting edge and machine are considered when transferring them to your machining task.
PCBN endmills for the joint geometry
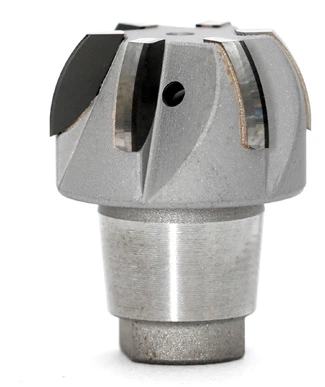
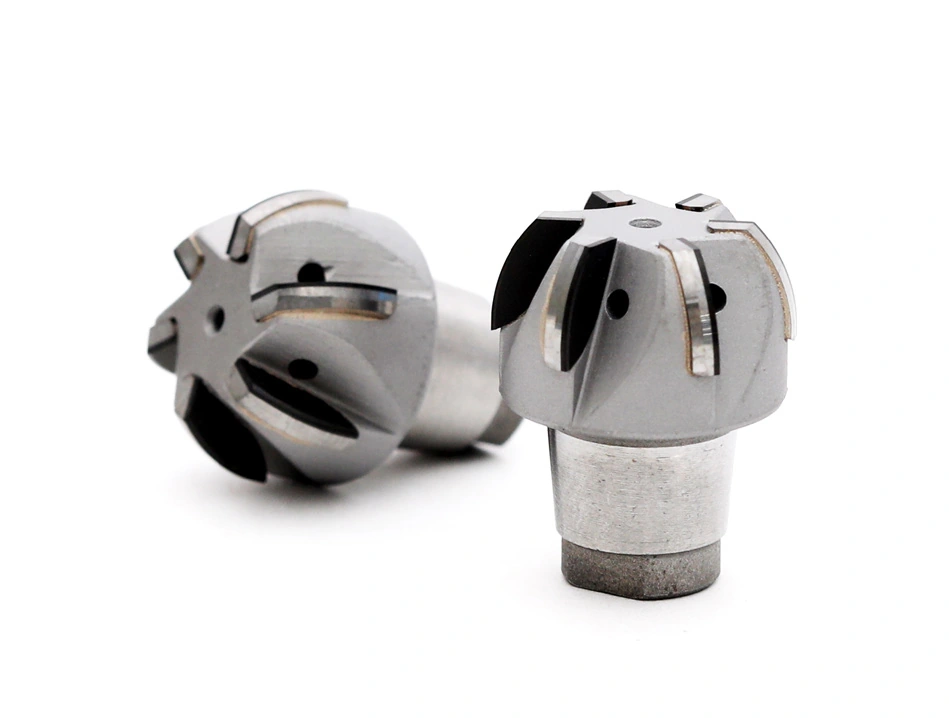
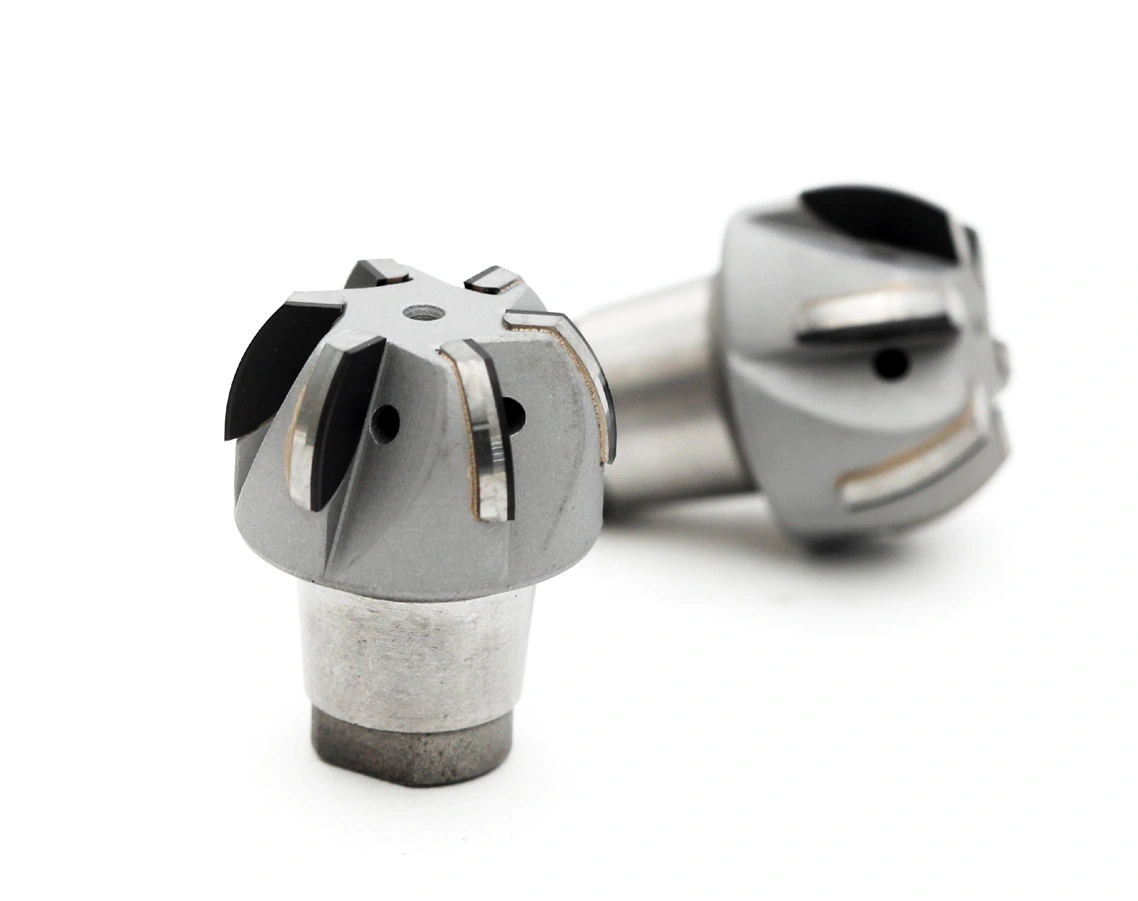
EHWA develops high-precision, high-quality PCBN endmills for CV-joint machining. The six-flute version introduced in the product sheet targets high tool life in high-speed machining. EHWA describes strong cutting performance and customised tooling solutions.
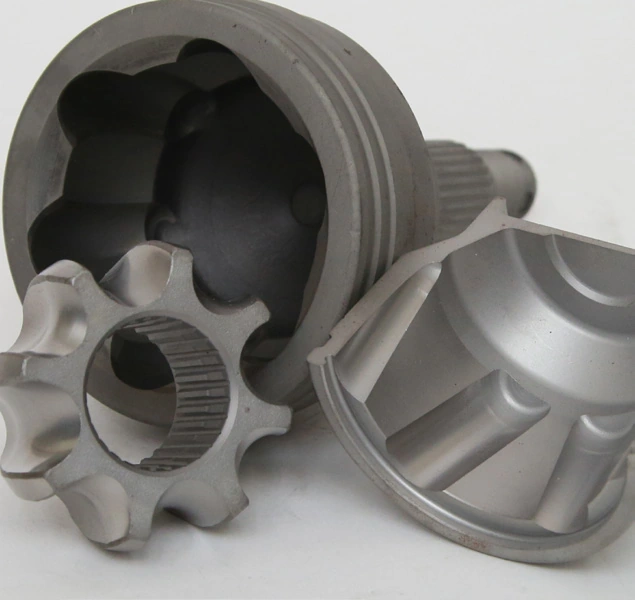
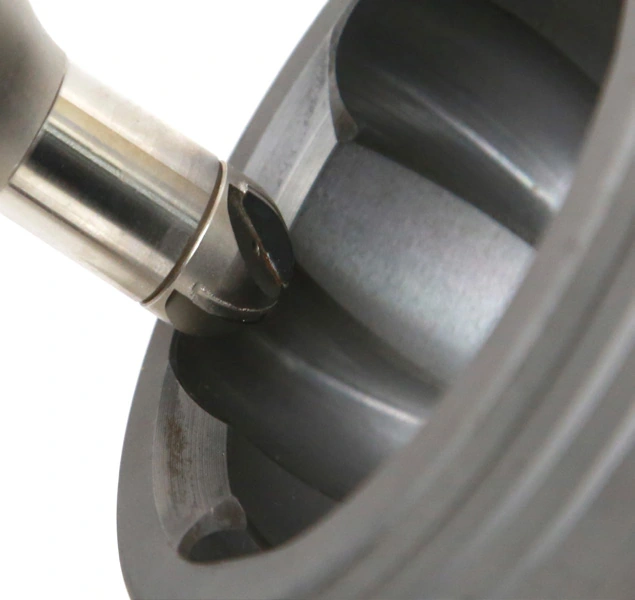
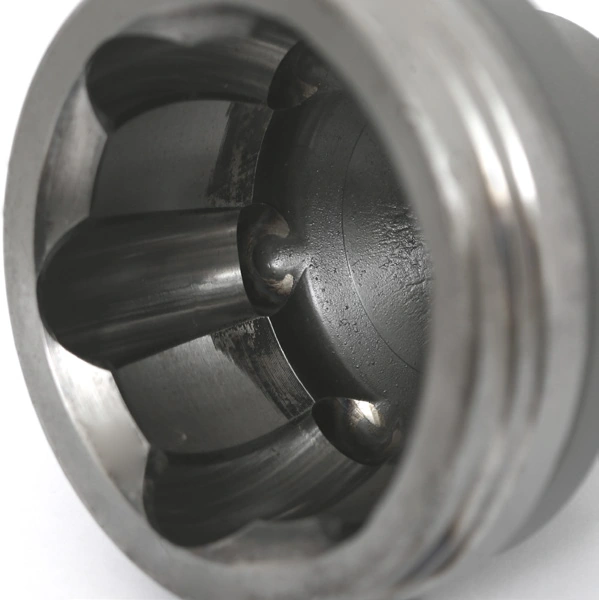
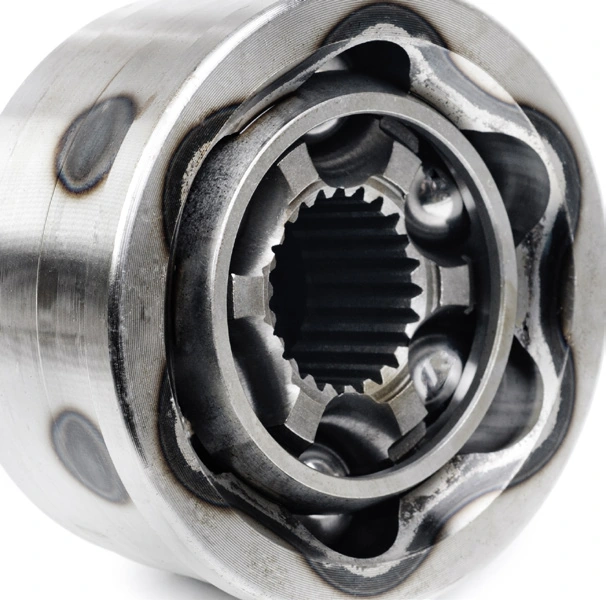
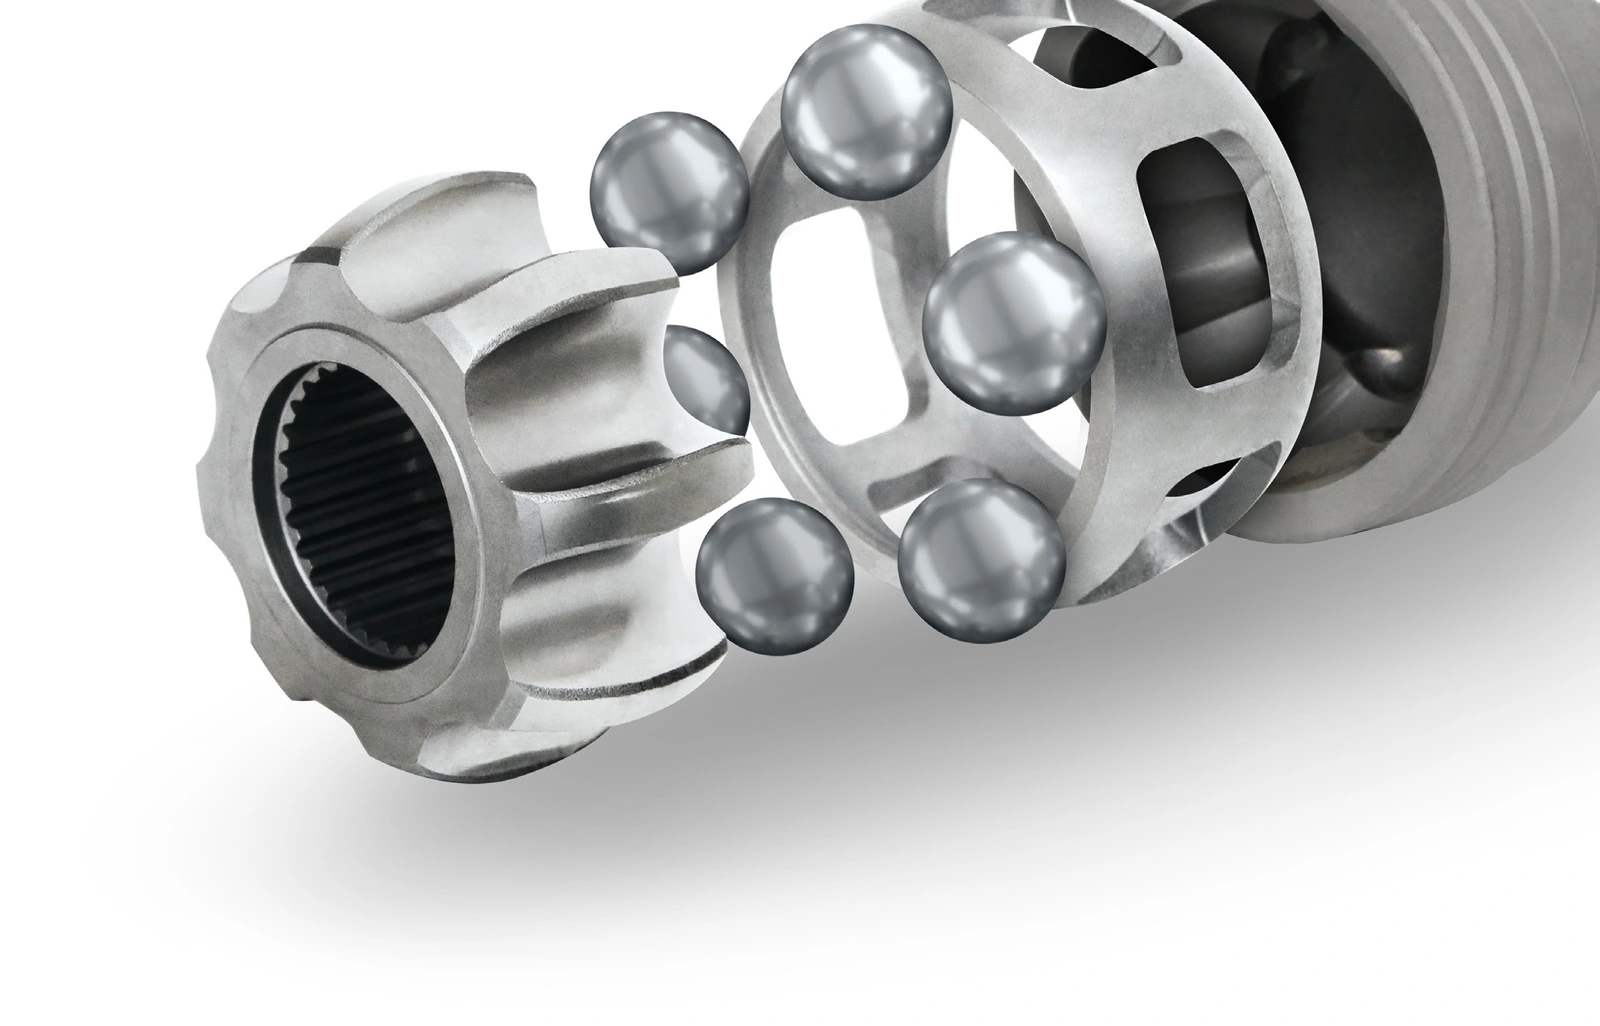
HFS12 with four or six flutes
| Parameter | Four-flute version | Six-flute version |
|---|---|---|
| Body type | HFS12 | HFS12 |
| Cutting material | PCBN | PCBN |
| Number of flutes | 4 F | 6 F |
| Design | See the four-flute tool view | See the six-flute tool view |

Endmill tool-life comparison
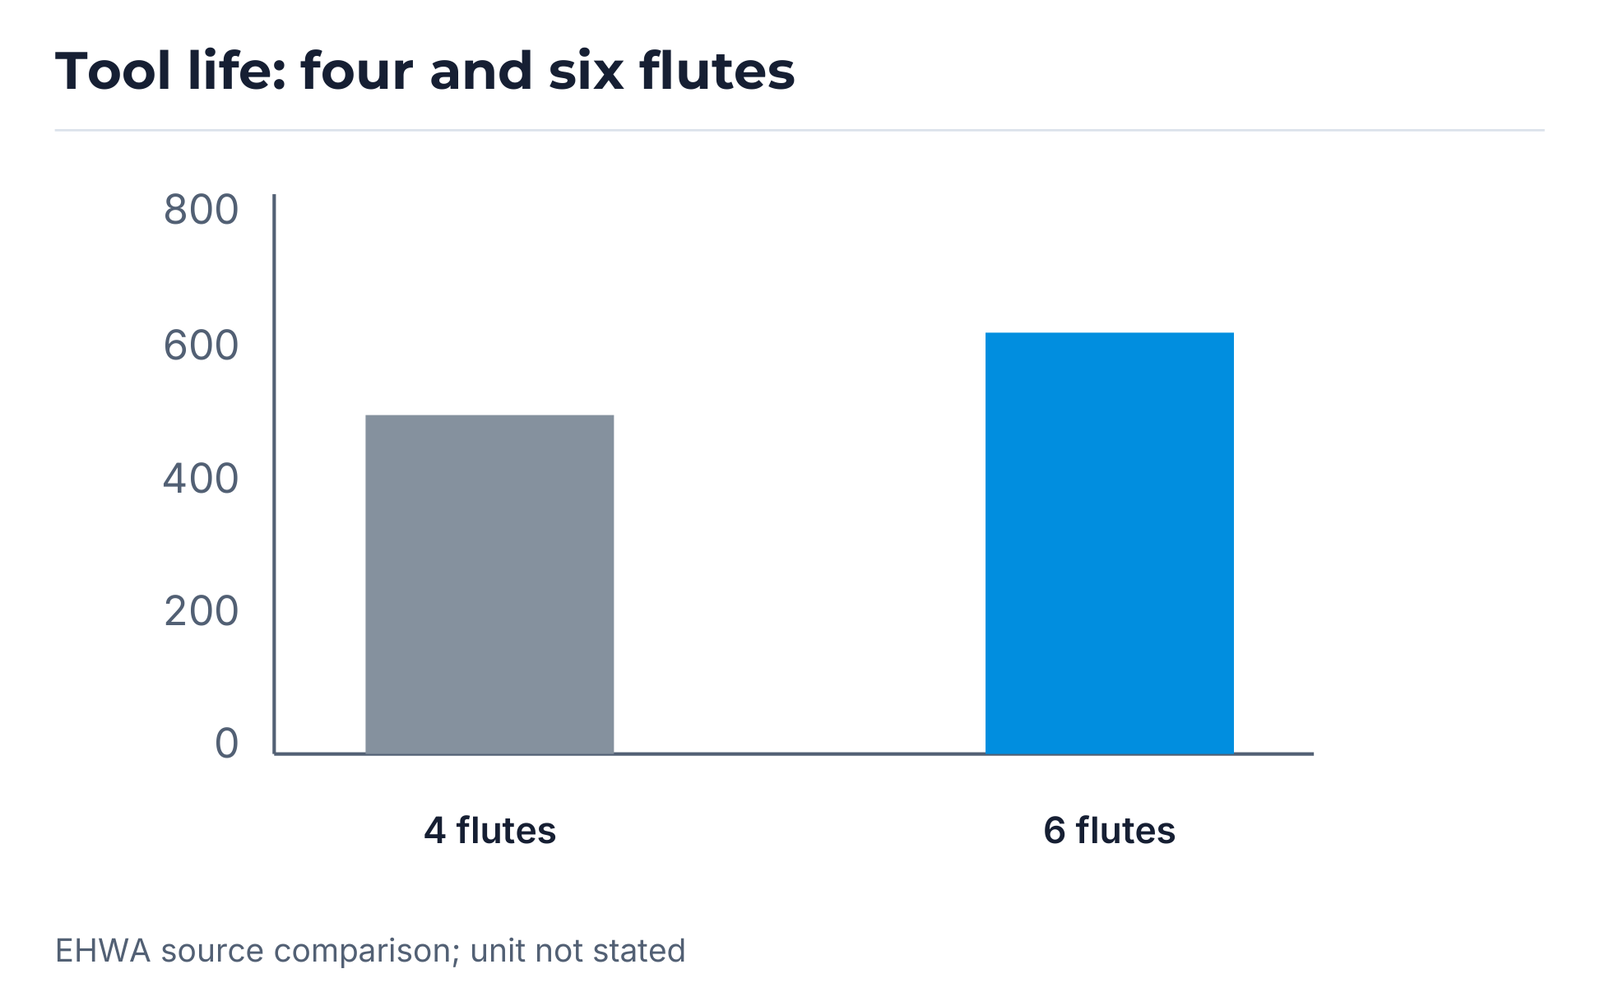
The EHWA chart compares the tool life of the four- and six-flute versions. The six-flute version has the higher bar. The original axis contains 0, 200, 400, 600 and 800. Neither a unit nor exact numerical bar labels are provided; the chart therefore retains the original bar proportions without adding minutes, component counts or a percentage improvement.
Develop your CV-joint tooling solution
EHWA offers customised endmill designs and tooling solutions to meet your requirements. Provide the component drawing, material and heat treatment, required contour, machine and tool holder. Add cut type, cutting speed, feed rate, depth of cut, coolant arrangement, surface requirements and current tool utilisation.
EHWA Europe: info@ehwadia.de · +49 6173 997780
Documents and edition
The technical basis comprises the complete one-page EHWA EBC52X CV-joint product sheet and the complete two-page EHWA PCBN endmill document. The endmill document bears the print date 06/2024; the EBC52X sheet does not state a print date. EHWA DIAMOND: since 1975. Editorial edition of this combined publication: 13 October 2026.