Coated PCBN grade for bearing steel
EHWA DIAMOND - since 1975
Match the grade to continuous cutting of bearing steel
EBC16S is a coated PCBN grade with low CBN content for continuous cutting of bearing steel. EHWA identifies SUJ2 and 100Cr6 as applications and describes the grade as providing strong performance even under demanding machining conditions. Cutting edge selection and cutting conditions are matched to material condition, component geometry and surface requirements.
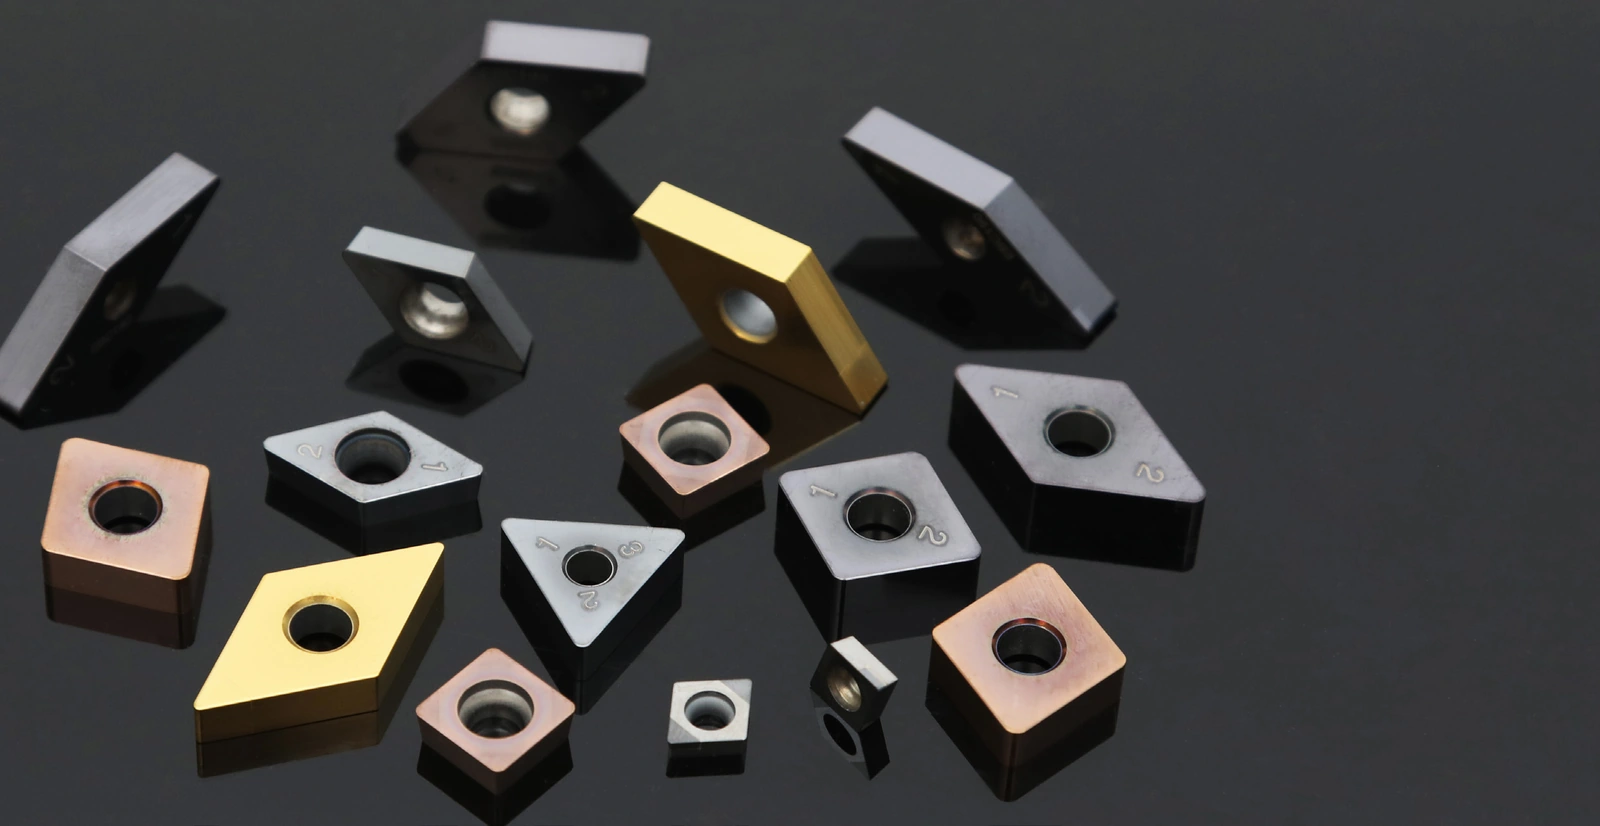
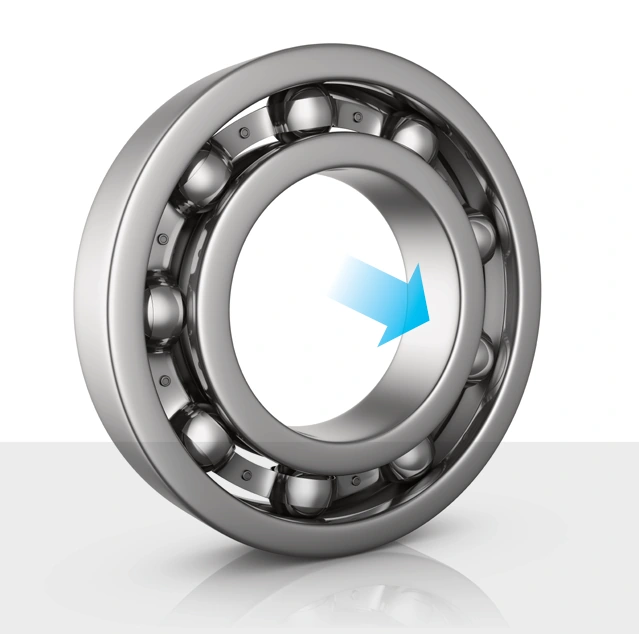
The product images show several insert shapes; the data sheet does not specify individual ordering codes, insert dimensions, coating composition or a numerical CBN content. EBC16S remains the grade designation.
Two cutting examples on SUJ2
Both examples use continuous wet cutting. The cutting data remain associated with their respective examples.
| Cutting parameter | Example 1 | Example 2 |
|---|---|---|
| Material | SUJ2 | SUJ2 |
| Cutting speed | 220 m/min | 200 m/min |
| Feed rate | 0.15 to 0.22 mm/rev | 0.20 mm/rev |
| Depth of cut ap | 0.10 to 0.20 mm | 0.10 to 0.15 mm |
| Coolant supply | wet | wet |
| Cutting mode | continuous | continuous |
Comparison charts from the cutting examples
The EHWA charts compare EBC16S with an unspecified competitor tool. In both cases, the EBC16S bar is higher. The first comparison axis shows 0, 200, 400 and 600; the second shows 0, 100, 200, 300 and 400. Neither an axis unit nor exact numerical bar labels are given. The charts are therefore reproduced without interpreting them as pieces, minutes or a percentage improvement in tool life.
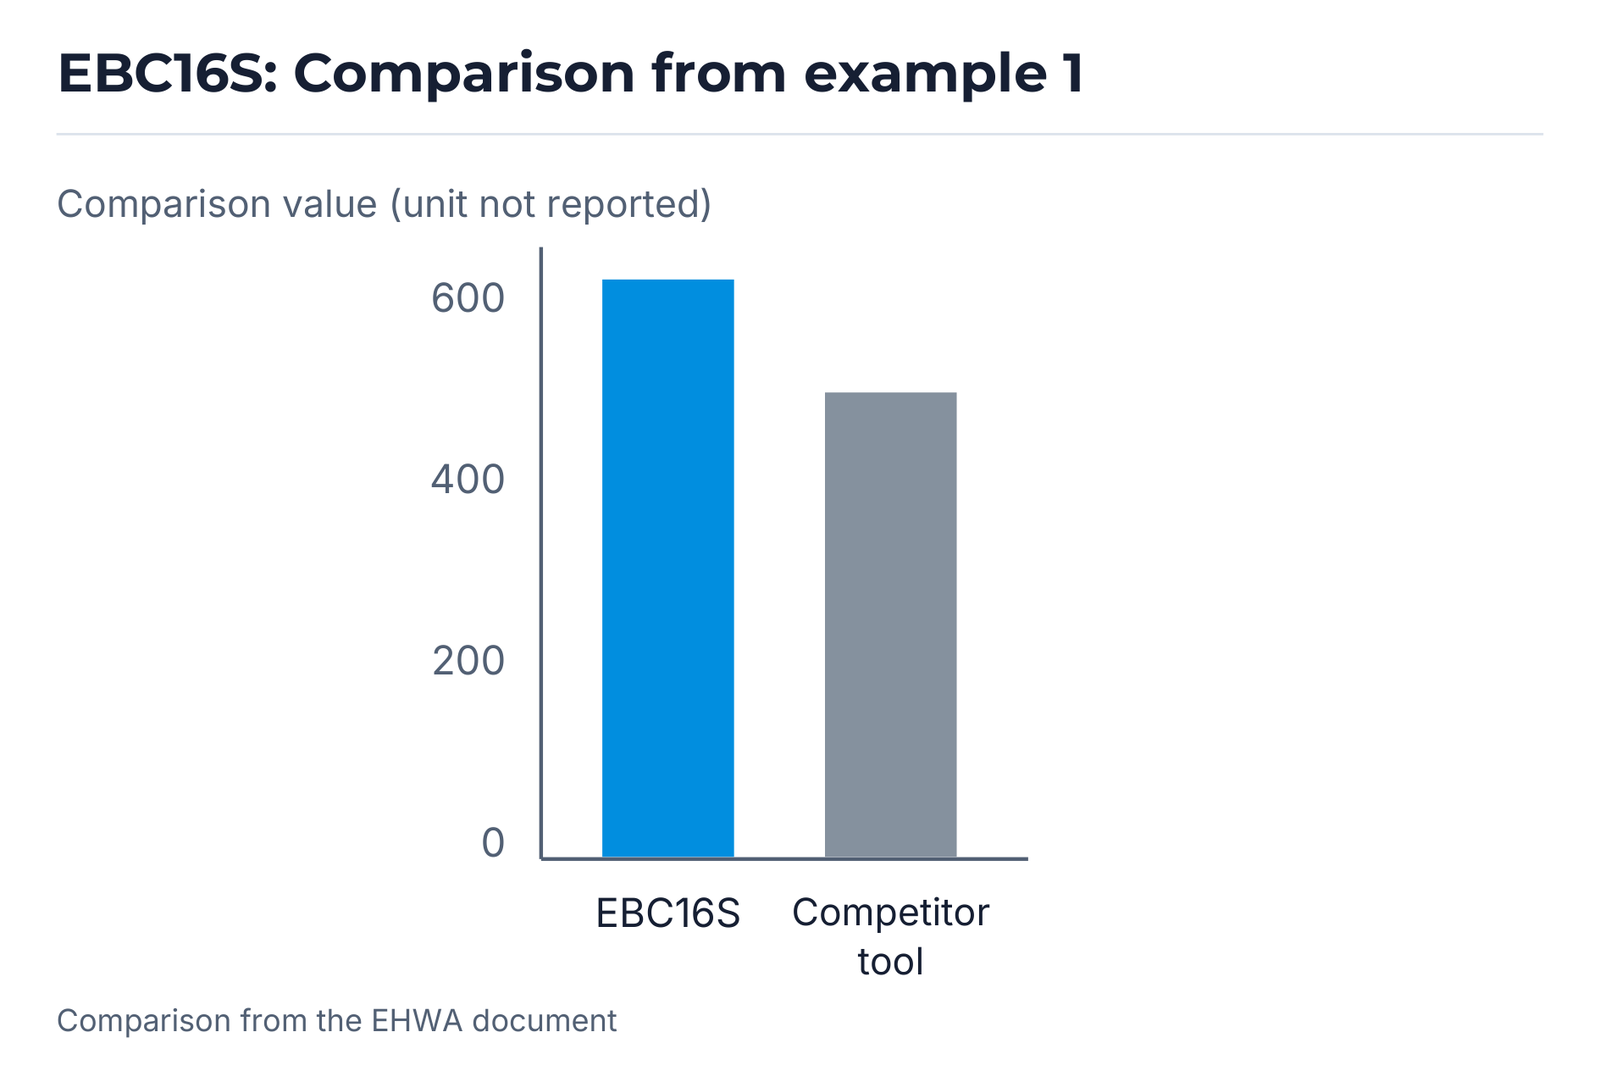
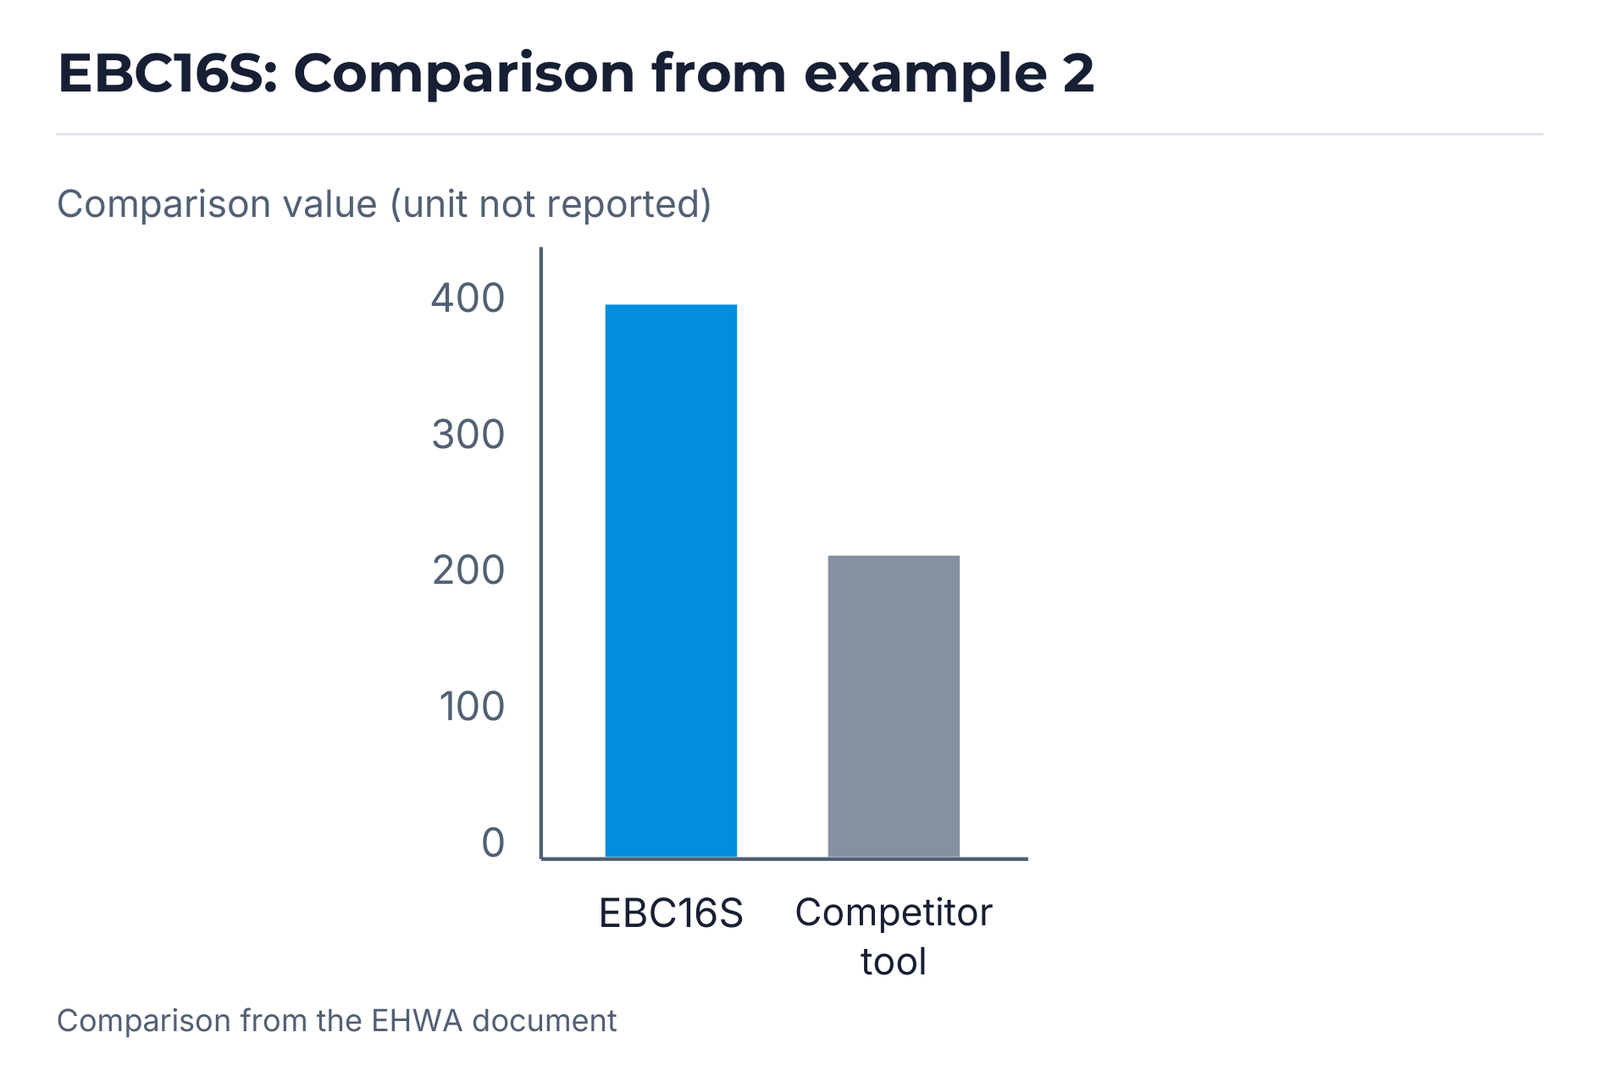
The charts belong to the two stated SUJ2 tests. The cutting data are application examples rather than general settings for every SUJ2 or 100Cr6 machining task.
Discuss your bearing-steel machining task
Provide the material and hardness, component drawing, existing insert shape and cutting edge design, machine and coolant arrangement. Add cutting speed, feed rate, depth of cut, surface requirements and current tool utilisation. This information supports matching EBC16S to your continuous cut.
EHWA Europe: info@ehwadia.de · +49 6173 997780
Editorial edition: 13 October 2026. Technical basis: the complete one-page EHWA EBC16S bearing-steel data sheet.